Oil Mist Collectors for Machine Tools
An oil mist collector has to catch something a dust filter was never designed for: a liquid aerosol of coolant droplets, sub-micron in the respirable range, which wets the media, drains, and — if the unit is built for dust — ends up in the ductwork instead of the sump.
0.19–0.25 mg/m³
inhalable metalworking fluid aerosol measured on machine operators
45%
of the exposure variation between operators explained by compressed air, enclosure or grinding
6% → 25%
of working time at peak exposure contributed a quarter of the average concentration
The window that goes grey by Friday
Oil mist is the contaminant people notice last, because it is invisible for the first few weeks. Then the windows go grey, the light fittings collect a film, and the benches feel tacky.
Metalworking fluid is sprayed at the cutting edge under pressure and at temperature, and a proportion of it becomes airborne as an aerosol — droplets in the respirable range that travel through the whole shop rather than settling around the machine. The exposure it causes is not minor: metalworking fluid aerosols are associated with occupational asthma, hypersensitivity pneumonitis and respiratory symptoms, and the UK has withdrawn the old threshold for fluid mist precisely because the earlier limits did not control those outcomes.
Two details decide how bad a machine shop gets. The first is whether the machine is enclosed. The second is how the chips and the settled mist are dealt with — because blowing a machine down with compressed air converts hours of settled fluid into a fresh aerosol in thirty seconds. Those two factors, plus grinding as a cutting task, accounted for about 45% of the differences in exposure between operators in a machine shop study.
What machine shop measurements show
0.19–0.25 mg/m³
Average inhalable aerosol measured on operators across five medium and large machine shops — with considerable variation between machines and between jobs.[1]
45%
Share of the between-operator exposure variation explained by three things: use of compressed air for cleaning, incomplete machine enclosure, and grinding as the cutting task. All three are design decisions.[1]
6% → 25%
Short-term peak exposures during 6% of the working time contributed about 25% of the average concentration — peaks, not the steady state, are where a mist collector earns its keep.[1]
0.1 mg/m³
The concentration at which a NIOSH risk assessment found significant lifetime risk of new-onset asthma and hypersensitivity pneumonitis under outbreak conditions, in fluid used mostly before 2000.[2]
Full sources are listed under References at the end of this page.
Enclose the machine, then catch it at the door
The best oil mist control is a closed machine. The second best is a collector connected to the enclosure so that the mist is captured where it is generated rather than after it has filled the shop. Everything else — airflow, media, drainage — is designed around those two facts.
Capture at the enclosure, at the right volume
Machine tools need a collector sized per machine or per machine group. FDOG-20P at 2,000 m³/h covers a single machine tool, FDOG-35P at 3,500 m³/h covers a larger machining centre or two machines, and FDOG-50P at 5,000 m³/h covers the heavier duty case or a group on one collector. The unit has to be ducted or bonneted to the machine enclosure — in the door line, not over it — because pulling from the wrong side just draws the mist across the operator.
Separate the liquid before it reaches the media
Coolant mist is a liquid, and a filter that fills with liquid stops passing air. The units deal with this in two ways: a rotating deflector strips the larger droplets out of the airstream before the media sees them, and the collected fluid drains back to the machine rather than sitting in the unit, with a level alarm so the sump is not forgotten. Cleaning is automatic on a differential-pressure setpoint across the range, because a machine tool that runs two shifts does not offer a convenient moment to stop and clean a filter.
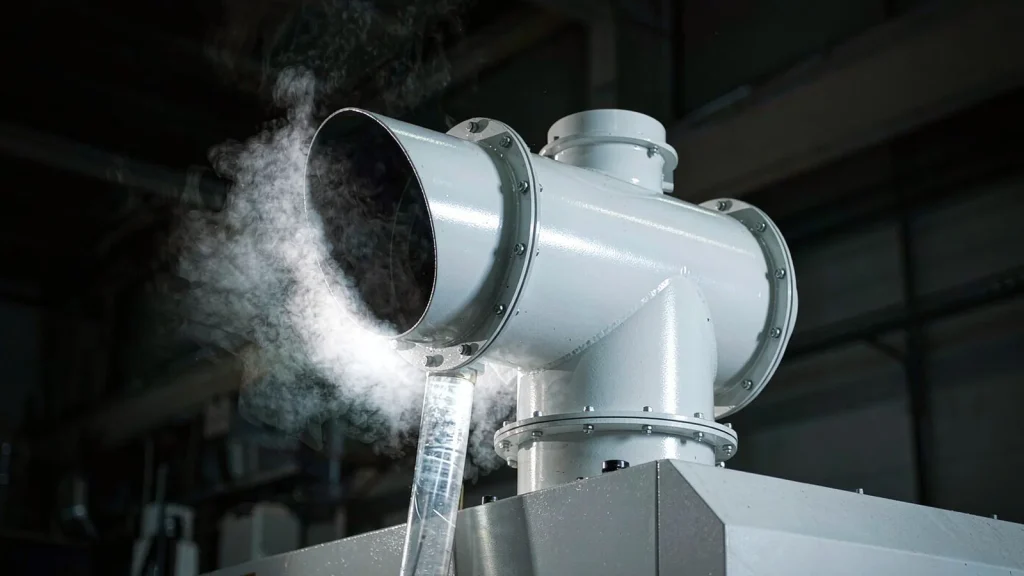
Oil mist collectors for machine tools
Three collectors cover a single machine tool through to a group of machines, from 2,000 to 5,000 m³/h. All of them separate the liquid before the cartridge.
What an oil mist installation includes
- A collector sized to the machine or machine group, with the connection arranged at the enclosure rather than over it
- Rotating deflector to strip coarse droplets before the media, and a drainage return to the machine sump
- Cartridge sets rated for liquid aerosol loading, plus spare first-stage media — this is the stage that loads first
- Commissioning with airflow verified at the machine connection and a walk-round of the shop to check the mist level where people actually stand
Send us the machine list, the coolant type and how the machines are cleaned down. Compressed-air blowdown changes the airflow a collector needs more than the spindle power does.
Machines and processes this covers
Precision machining and turning centres, automotive powertrain and component machining, medical device manufacture, mould and die machining, aerospace subcontract machining, EDM and grinding machines, and toolrooms. Coolant types covered include straight oils, soluble oils, synthetics and semi-synthetics — all four aerosolise, and the droplet loading differs enough to change the media specification. Where the process is dry machining or grinding of metal or composites, the hazard is dust rather than mist and the grinding dust pages are the better starting point.
At the machine
Questions from machine shop managers
Send us the machine list and the coolant type
Send us the machine list with spindle hours, the coolant type, whether compressed air is used for cleaning, and the shop layout. We will come back with the collector size per machine group, the connection arrangement and the media specification.
References
- Lillienberg L, Burdorf A, Mathiasson L, Thörneby L. Exposure to metalworking fluid aerosols and determinants of exposure. Ann Occup Hyg 2008. doi:10.1093/annhyg/men043 pubmed.ncbi.nlm.nih.gov
- Park RM. Risk assessment for metalworking fluids and respiratory outcomes. National Institute for Occupational Safety and Health (NIOSH). pmc.ncbi.nlm.nih.gov
- Occupational Safety and Health Administration (US). Metalworking fluids: safety and health best practices manual — exposure limits for mineral oil mist and metalworking fluid aerosol, and associated health effects. osha.gov
- Health and Safety Executive (UK). Controlling airborne contaminants at work: a guide to local exhaust ventilation. HSG258, 3rd ed. — Table 9 capture velocities for welding fume, and the commissioning checks for a moveable extraction arm. hse.gov.uk