Plasma Cutting Fume Extraction
Plasma cutting fume extraction is harder than welding fume extraction for one reason: the fume generation rate climbs steeply with arc current, and stainless plasma cutting produces more hexavalent chromium per minute than welding does. Sized on the bed and the current, it is manageable. Sized on the shop floor area, it is not.
16.5 → 119 mg/min
fume generation rate measured from 20 A to 50 A of plasma arc
219.8–480 µg/min
hexavalent chromium emitted by stainless plasma cutting
96–235 nm
geometric mean particle size — fine enough to travel across a cutting hall
A hotter arc makes a finer, faster fume
A plasma torch does not burn the plate, it melts it and blows the molten metal out of the kerf. The fume that leaves the cut is metal vapour that has already condensed, and it leaves hot.
Cutting shops tend to size extraction on the hall, because the hall is what you can see. The measurements say otherwise: fume generation from plasma cutting rises more than sevenfold as arc current goes from 20 A to 50 A, so a machine running thicker plate produces several times the fume of the same machine running thin sheet. A hood that was adequate on 6 mm plate is not adequate on 25 mm, even though the table, the hall and the operator have not changed.
The other variable is the material. Stainless plasma cutting puts hexavalent chromium into the plume at rates higher than welding fume measured in comparable studies, and the particles are fine — a geometric mean between about 96 and 235 nm, with a multimodal distribution. Fine particles do not settle; they follow the air across the shop, which is why capture at the cut matters more than dilution in the hall.
Fume generation against arc current
16.5 → 119 mg/min
Total fume generation rate measured from stainless plasma cutting as arc current rose from 20 A to 50 A — arc current was the dominant factor in fume emission, ahead of any other cutting parameter.[1]
219.8–480 µg/min
Hexavalent chromium emission rate from the same cutting trials — higher than welding fume measured in earlier work on the same equipment class.[1]
96–235 nm
Geometric mean size of the fine particle fraction, confirmed by both size measurement and electron microscopy. A multimodal distribution means the coarse cut dust is not the fraction to design for.[1]
R = 0.93
Correlation between nitrogen oxides and hexavalent chromium formation in plasma cutting fume — evidence that the Cr(VI) is created in the oxidation zone at the arc, which is exactly where the hood has to be.[1]
Full sources are listed under References at the end of this page.
Size on the bed area and the amps
Plasma extraction is designed from two numbers: the bed area the fume has to be pulled out of, and the arc current the machine runs at. Everything else — hood shape, duct routing, collector size — follows from those two.
Downdraft through the table, capture at the kerf
On a cutting table the primary control is downdraft or backdraft at the cut, because the plume is created at bed level and rises. The extraction volume scales with bed area rather than with the number of torches, which is why the range for table duty spans 10,500 m³/h (FDYC-80Z) up to 30,000 m³/h (FDZY-30P). Slag and spatter come with the fume on a plasma table, so the first stage has to be designed for hot particles — a spark arrestor and a drop-out section ahead of the cartridge, not a cartridge straight off the duct.
Where the bed is too big for a hood, use the hall
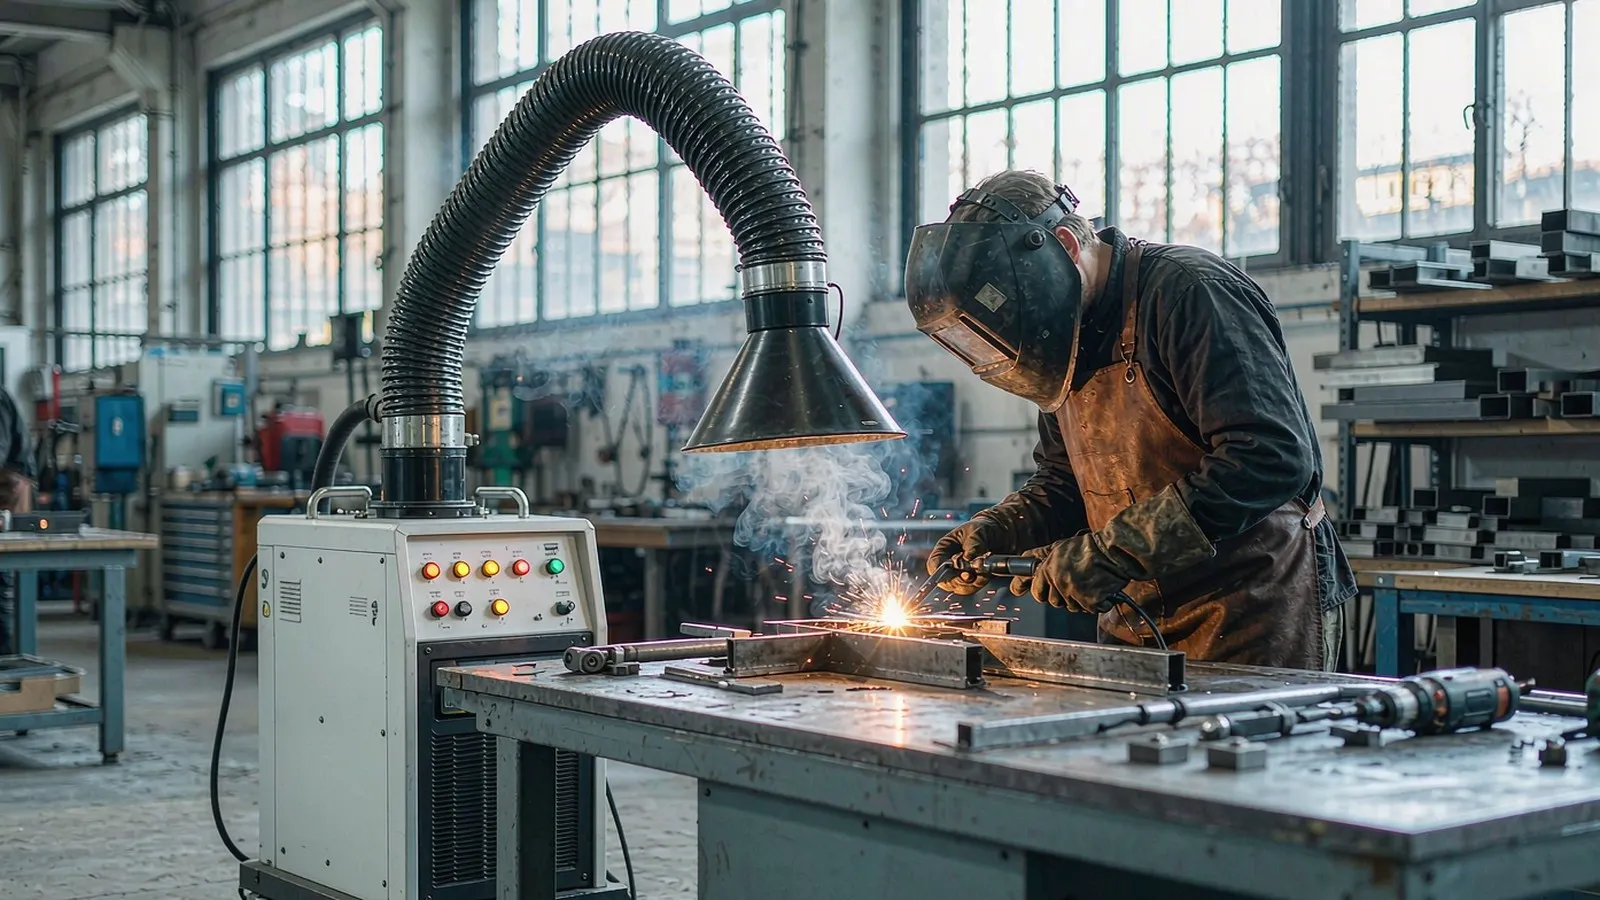
Long beds and multiple tables in one bay are where blow-suction comes in. FDCX-20P at 20,000 m³/h and FDCX-30P at 30,000 m³/h create a controlled air path across the cutting zone, pushing clean air from one side and pulling contaminated air away on the other, which lets a large hall be controlled without a hood over every metre of bed. Where a single machine runs high current on thick plate, local extraction with FDZY-10P (12,000 m³/h), FDZY-15P (17,000 m³/h) or FDZY-20P (22,000 m³/h) combined with a table hood usually gives better capture per kilowatt than treating the whole bay.
Downdraft tables, local hoods and blow-suction
Seven units cover a single table through to a hall: local downdraft extraction at one end of the range, ducted central collectors at the other, and blow-suction for long beds. All filter to 0.3 µm.
What a plasma table installation includes
- Downdraft or backdraft table extraction, or a hood arrangement at the cutting head where the table cannot be modified
- Spark arrestor, drop-out section and a first stage rated for hot particles and slag, ahead of the cartridge
- Ducting, balancing dampers and discharge arrangement where a central collector serves more than one table
- Commissioning with capture velocity measured at the cut and airflow verified at each extraction point, at the current you actually cut at — not at a light setting
Tell us the bed dimensions, the plate thickness range and the arc current. Plate thickness and current together set the airflow; quoting from the hall size is how plasma systems end up undersized.
Cutting shops this fits
Steel service centres, structural steel fabrication, shipbuilding and offshore fabrication, heavy engineering, pressure vessel and tank shops, and general profiling shops running one or more plasma tables. Hand-held plasma cutting in a maintenance bay is a different case — that is better served by a mobile unit with a hood at the cut, which the manual welding and wall mounted pages describe. Where the process is laser rather than plasma, the plume is finer again and needs different filtration stages.
At the table
Questions from cutting shop managers
Send us the bed size and the plasma current
Send us the bed dimensions, the plate thickness range, the arc current and the cutting hours per shift. We will come back with the capture arrangement, the airflow and the collector size — and where the bed is long, the blow-suction layout as an alternative.
References
- Wang J, Hoang T, Floyd EL, Regens JL. Characterisation of particulate fume and oxides emission from stainless steel plasma cutting. Ann Work Expo Health 2017;61(3):311–320. doi:10.1093/annweh/wxw031 stacks.cdc.gov
- Health and Safety Executive (UK). Controlling airborne contaminants at work: a guide to local exhaust ventilation. HSG258, 3rd ed. — Table 9 capture velocities for welding fume, and the commissioning checks for a moveable extraction arm. hse.gov.uk
- Health and Safety Executive (UK). EH40/2005 Workplace exposure limits — hexavalent chromium compounds, nickel and zinc oxide. hse.gov.uk
- WorkSafe Queensland (AU). Welding — hazards and controls, code of practice 2021. worksafe.qld.gov.au
- IARC Working Group. Welding, molybdenum trioxide, and indium tin oxide. IARC Monographs on the Evaluation of Carcinogenic Risks to Humans, Volume 118, 2018. Summary: Guha N, et al. The Lancet Oncology 2017;18(5):581–582. doi:10.1016/S1470-2045(17)30255-3
- Health and Safety Executive (UK). Change in enforcement expectations for mild steel welding fume. Safety alert STSU1-2019. hse.gov.uk